Description
1. Product Overview
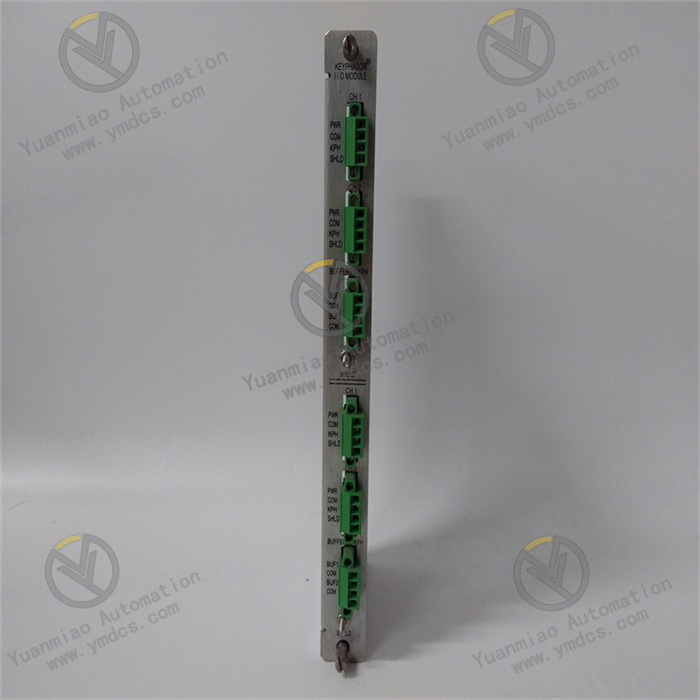
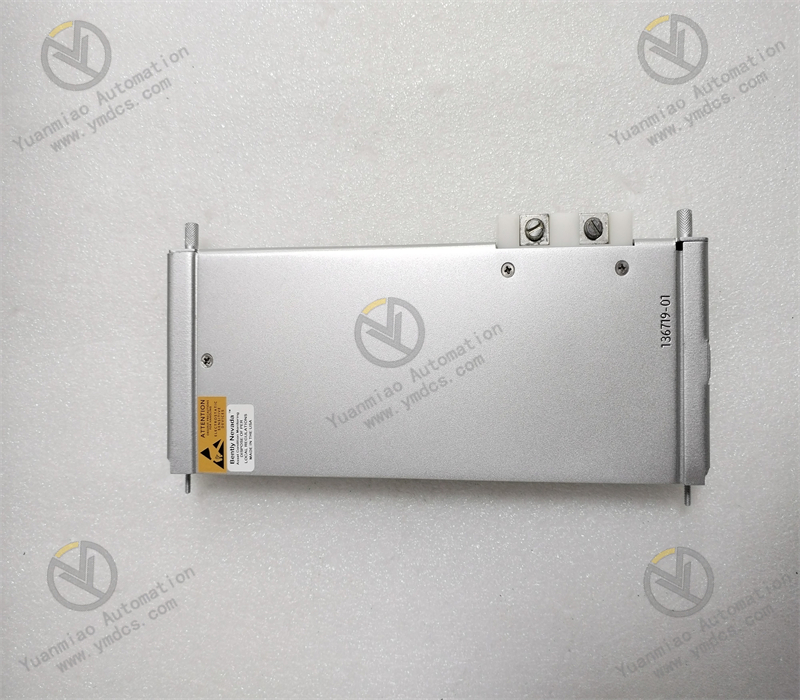
Bently Nevada 136719-01 is an original built-in intrinsic safety isolation barrier module for 3500/04 manufactured by Baker Hughes Bently Nevada. It is a dedicated core supporting module of the 3500 series TSI machinery condition monitoring and protection system, designed for monitoring rotating machinery in flammable and explosive hazardous areas such as chemical, oil & gas and petrochemical industries. As the core intrinsic safety explosion-proof unit of the system, the module integrates built-in isolation barriers. It can directly provide intrinsic safety signal isolation and explosion-proof protection for eddy current sensors, vibration sensors and speed keyphase sensors deployed in hazardous areas. It blocks energy conduction between hazardous and safe areas at hardware level and eliminates explosion risks caused by electric sparks. It serves as critical supporting hardware for safe and stable operation of unit TSI monitoring systems under explosion-proof working conditions.
The 136719-01 is an upgraded integrated intrinsic safety isolation module of the 3500/04 series. Different from traditional external isolators, it adopts a rack-integrated half-height structure, requiring no additional external explosion-proof isolation devices and greatly simplifying on-site wiring and cabinet layout. Equipped with high-precision passive isolation loops, energy limiting circuits and lossless signal transmission architecture, it fully meets intrinsic safety explosion-proof standards while preserving the original accuracy of sensor signals to the maximum extent with no signal attenuation, waveform distortion or phase shift. The complete unit has passed factory explosion-proof certification, high-low temperature aging, EMC, vibration and shock reliability tests. It is suitable for flammable and explosive hazardous conditions of Zone 0, Zone 1 and Zone 2 in industry. It is widely used in explosion-proof monitoring modification of units for oil & gas production, refining units, chemical stations and coal chemical projects, replacement of old external isolation systems, explosion-proof matching for 3500 TSI systems and stocking of core industrial control explosion-proof spare parts.
2. Functional Features
Intrinsic safety explosion-proof isolation for compliant protection in hazardous areas Built with dedicated intrinsic safety isolation barriers and precision energy limiting circuits, the module complies strictly with industrial intrinsic safety explosion-proof specifications. It effectively limits voltage, current and energy transmitted from safe areas to hazardous areas, thoroughly eliminating potential safety hazards from electrical overload, leakage and electric sparks. It is perfectly applicable to equipment monitoring scenarios with flammable and explosive gas and dust. It can directly connect to various intrinsic safety vibration, displacement and speed sensors installed in hazardous areas to realize safe acquisition and transmission of equipment signals in hazardous zones. It replaces conventional external isolators and avoids problems such as complicated wiring, redundant protection and explosion-proof failure of external equipment, ensuring compliant, safe and stable operation of TSI systems under explosion-proof conditions.
Lossless isolated signal transmission with no loss of monitoring accuracy Adopting passive high-precision isolated transmission architecture, it overcomes the signal attenuation defect of ordinary isolation modules. It achieves electrical isolation and energy blocking while completing lossless transmission of sensor signals. Specially optimized for weak high-frequency signals from eddy current probes, keyphase pulse signals and vibration analog signals, it delivers transmission advantages of ultra-low insertion loss, no phase delay and no waveform distortion. It fully retains raw monitoring data of tiny equipment vibration, subtle shaft displacement and low-speed pulses, without affecting the monitoring accuracy, protection logic and fault diagnosis performance of the original TSI system, balancing explosion-proof protection and high-precision monitoring.
Integrated rack-mounted design to simplify on-site O&M layout It adopts the standard half-height integrated structure of the 3500 series, which can be directly inserted into the slots of the 3500 system rack and used together with main control and monitoring modules. No separate installation of external isolators, extra fixing brackets or redundant wiring is required. Compared with traditional distributed explosion-proof isolation schemes, it greatly reduces cabinet occupation space, simplifies on-site wiring procedures and lowers wiring failure points and hidden risks. The standardized integrated design is compatible with the full rack architecture of the 3500 series with plug-and-play feature and strong adaptability, enabling rapid integrated technical upgrading of old external explosion-proof systems.
Strong anti-interference electrical isolation for stable operation under harsh conditions The module adopts full electrical isolation design together with multi-stage EMI filtering and noise reduction circuits. It can effectively isolate electromagnetic harmonics and power frequency interference generated by power cables, frequency converters and contactors in safe areas, and block cross-region signal crosstalk and clutter conduction. It meets energy isolation requirements for explosion protection and avoids signal jump, data drift and false alarms caused by strong electromagnetic interference in industrial sites. It guarantees authenticity, continuity and stability of monitoring signals for equipment in hazardous areas, adapting to complex explosion-proof industrial conditions featuring high temperature & humidity, dust, oil contamination, continuous vibration and strong electromagnetic interference.
Hardware-based status self-diagnosis for accurate fault tracing Embedded with full-coverage hardware status monitoring mechanism, it monitors the status of module isolation loops, operating conditions of energy limiting units, signal transmission links, power supply status and hidden hardware faults 7×24 hours in real time. It accurately identifies loop abnormality, signal overload, isolation failure and line faults, automatically generates fault codes and uploads them to the 3500 upper system and System1 diagnosis platform. Operation and maintenance personnel can quickly complete troubleshooting, loop verification and hidden danger rectification, greatly shortening the repair time for explosion-proof system faults and avoiding unit safety risks arising from isolation failure. The module supports in-situ hot-swap replacement without shutdown, power cut or system parameter reconstruction, delivering extremely convenient operation and maintenance.
- Industrial explosion-proof rugged design for long-term maintenance-free operation The module features industrial rugged structure. Its PCB board is coated with military-grade three-proof coating, offering excellent moisture-proof, dust-proof, corrosion-resistant, vibration-resistant and temperature cycle resistant performance. It can withstand harsh operating conditions inside explosion-proof cabinets for a long time. All core components pass rigorous factory screening, aging calibration and explosion-proof compatibility tests. With no high-frequency vulnerable parts, low power consumption and low heat generation, it supports 7×24-hour uninterrupted continuous energized operation all year round. No attenuation of isolation performance or deviation in signal transmission occurs during long-term operation, requiring no frequent calibration and routine maintenance to meet demands for long-term stable operation of industrial equipment.
3. Technical Specifications
3.1 Core Adaptation Parameters
Product Model: 136719-01 Product Series: Bently Nevada 3500/04 Built-in Intrinsic Safety Isolation Barrier Module Brand: Bently Nevada (Baker Hughes) Product Type: Rack-integrated intrinsic safety explosion-proof isolation module Compatible Systems: Full-series Bently Nevada 3500 Machinery Condition Monitoring and Protection System Applicable Equipment: Rotating machinery in explosion-proof areas including steam turbines, compressors, fans and pump sets in oil & gas, chemical and petrochemical industries Compatible Sensors: Full range of Bently Nevada intrinsic safety eddy current displacement, vibration and speed keyphase sensors Core Functions: Intrinsic safety explosion-proof isolation for hazardous areas, electrical energy limitation, lossless isolated transmission of sensor signals, electromagnetic interference shielding, hardware status self-diagnosis, explosion-proof supporting for TSI systems Application Scenarios: Unit monitoring in flammable and explosive hazardous areas, explosion-proof renovation of TSI systems, integrated replacement of external isolators, system complete-set for chemical and oil & gas projects, stocking of explosion-proof industrial control spare parts
3.2 Signal and Isolation Parameters
Isolation Method: Built-in intrinsic safety passive electrical isolation with precise energy limitation Transmission Signals: Compatible with full-range analog / pulse sensing signals for vibration, displacement, speed and keyphase Transmission Performance: Ultra-low insertion loss, no phase shift, no waveform distortion, zero data attenuation Anti-interference Capability: Multi-stage EMI filtering to eliminate electromagnetic crosstalk, power frequency clutter and signal jump Fault Identification: Self-check and alarm for isolation loop abnormality, signal overload, line faults and hardware failure
3.3 Electrical Operating Parameters
Operating Power Supply: Standard DC power supply for 3500 racks, integrated power intake from rack Operating Power Consumption: Ultra-low power design, low heat generation and stable operation of the whole unit Electrical Architecture: Complete electrical isolation between safe area and hazardous area with one-way energy blocking protection Explosion-proof Grade: Complies with industrial intrinsic safety explosion-proof standards, applicable to multiple types of flammable and explosive conditions Operating Characteristics: No parameter drift or attenuation of isolation performance during long-term energized operation
3.4 Mechanical and Installation Parameters
Structure Type: Standard half-height compact integrated module of 3500 series Installation Method: Embedded installation in standard slots of 3500 rack, plug-and-play Fixing Method: Cabinet snap lock for seismic anti-loosening, easy assembly and disassembly Protection Coating: Full-board military-grade three-proof coating, moisture-proof, dust-proof, corrosion-resistant and anti-aging Replacement Feature: Non-destructive in-situ replacement of old external isolation equipment and faulty modules; no rewiring, configuration reconstruction or parameter calibration required
3.5 Environmental Operating Parameters
Operating Temperature: -20℃~+60℃, standard temperature range for industrial TSI systems Storage Temperature: -40℃~+85℃ Operating Humidity: 5%~95%RH (non-condensing) Environmental Resistance: Applicable to flammable and explosive hazardous conditions; resistant to strong electromagnetic interference, vibration shock, temperature alternation, dust and corrosion Operation Mode: Supports 7×24-hour uninterrupted continuous energized operation all year round
4. Hardware Configuration & Structural Advantages
4.1 Core Hardware Configuration
The Bently Nevada 136719-01 module adopts dedicated intrinsic safety explosion-proof isolation hardware architecture for 3500/04. It is equipped with precision energy limiting units, passive isolation transmission loops, multi-stage EMI noise reduction filter circuits, hardware status self-diagnosis units and signal shaping matching circuits. All core components have passed Baker Hughes factory explosion-proof certification, rigorous screening, high-low temperature aging and EMC tests, tailored for safe transmission of weak sensor signals under hazardous area conditions. The module adopts partitioned isolation hardware design to strictly separate electrical loops of safe areas and hazardous areas, precisely limiting cross-region transmission energy and eliminating explosion-proof hidden dangers at hardware source. Meanwhile, it is equipped with adaptive signal matching circuits compatible with signal parameters of full-range Bently Nevada sensors to guarantee lossless and high-precision transmission of various monitoring signals. Its hardware explosion-proof reliability and signal stability surpass traditional external isolators.
4.2 Structural Design Advantages
The module features an industrial-grade compact half-height integrated structure perfectly matching standard slots of 3500 series racks, with high integration and minimal cabinet footprint. It thoroughly solves pain points of traditional external isolation equipment such as messy wiring, large space occupation and numerous failure points. The reinforced PCB substrate has high structural strength. Combined with rack snap-lock mounting structure, it can withstand continuous cabinet vibration, impact during equipment start-stop and cabinet temperature alternation for a long time, preventing common faults such as module loosening, poor contact and intermittent signal disconnection. The full-board military-grade three-proof coating effectively protects against erosion from cabinet moisture, dust, oil stains and corrosive gas to maintain long-term stable explosion-proof isolation performance. With native standardized system compatibility, it seamlessly works with all monitoring and protection modules of the 3500 series. In-situ replacement requires no wiring modification, program reconstruction or parameter re-tuning, substantially cutting costs for explosion-proof system technical transformation, maintenance and spare parts.
5. Working Principle
The Bently Nevada 136719-01 (3500/04) intrinsic safety isolation module implements a full closed-loop working mechanism: hazardous area signal access → energy limiting isolation → electromagnetic filtering and shaping → lossless signal transmission → hardware status self-diagnosis → safety closed-loop protection. It serves as the core safety isolation unit of TSI unit monitoring systems under explosion-proof working conditions.
During system operation, the module receives raw operating condition signals such as vibration, displacement and speed pulse collected by various sensors installed in flammable and explosive hazardous areas in real time. Through built-in precision energy limiting and passive isolation loops, it strictly blocks transmission of high voltage and large current energy from safe area cabinets to hazardous areas. The cross-region electrical energy is controlled within explosion-proof safety thresholds to eliminate explosion risks caused by electric sparks and electrical overload. Meanwhile, multi-stage EMI filtering and waveform shaping circuits remove industrial electromagnetic clutter, power frequency interference and invalid noise signals. It restores pure and stable equipment operating condition signals without loss of raw monitoring data, completely retaining characteristics of tiny changes in equipment operating status.
The standardized signals after isolation, filtering and shaping are transmitted losslessly to 3500 series monitoring modules and main control systems to support unit condition monitoring, fault diagnosis and action of over-limit protection logic. The module performs real-time self-inspection of isolation loop operating conditions, status of energy limiting units, integrity of signal transmission links and hardware operating conditions throughout operation. It accurately identifies hidden risks such as loop abnormality, signal overload and isolation failure, promptly generates fault codes and uploads alarms. Together with the TSI system, it executes fault tolerance and safety interlock to fully guarantee intrinsic safety and operational stability of rotating machinery monitoring systems in explosion-proof areas.
6. Application Scenarios
Explosion-proof monitoring of units in flammable and explosive hazardous areas Widely applied to hazardous conditions with flammable and explosive gas and dust such as oil, natural gas, fine chemical, coal chemical and refining facilities. It adapts to 3500 series TSI monitoring systems for rotating machinery including steam turbines, centrifugal compressors, process fans and key pump sets in such areas. With intrinsic safety isolation and explosion-proof functions, it realizes safe acquisition and precise monitoring of equipment sensor signals in hazardous areas, meets safety specifications of industrial control systems in explosion-proof zones, and guarantees monitoring continuity and operation safety of units under high-risk conditions.
Integrated technical upgrading of traditional external isolation systems Aiming at problems of conventional external isolators on site including complicated wiring, numerous failure points, large space occupation, high signal loss and unstable explosion-proof performance, hardware upgrading can be implemented with this integrated intrinsic safety module. The rack-integrated isolation scheme replaces distributed external equipment to simplify cabinet layout, reduce wiring faults and improve signal transmission accuracy and explosion-proof stability, completing intelligent and integrated technical renovation of old explosion-proof monitoring systems at low cost and high efficiency.
Complete-set matching and maintenance of explosion-proof TSI systems As the core supporting isolation unit of 3500 explosion-proof TSI systems, it can be used together with full-range monitoring modules and main control modules to form standardized machinery protection systems. It meets complete-set demands of unit monitoring systems for new chemical and oil & gas projects. Meanwhile, it solves on-site problems such as aging, performance degradation and signal abnormality of explosion-proof isolation modules, ensuring long-term compliant and stable operation of monitoring systems.
- Stock of core explosion-proof spare parts for high-risk industrial equipment As the original intrinsic safety explosion-proof isolation module of Bently Nevada 3500 system, it acts as essential maintenance spare parts for high-risk units of oil & gas, chemical and coal chemical enterprises. It can rapidly handle on-site emergencies including isolation failure, abnormal signal transmission and loop faults, preventing equipment damage, unit shutdown and safety accidents caused by monitoring failure due to explosion-proof isolation faults, and securing uninterrupted safe and stable operation of high-risk production equipment all year round.